

Choosing the right water filling machine is one of the most important decisions for any bottled water producer. Whether you are launching a new mineral water brand or upgrading an existing production line, the equipment you select will directly affect product quality, operational efficiency, hygiene standards, and long-term profitability.
In today’s competitive beverage market, buyers are no longer looking for standalone machines. They are looking for integrated, intelligent systems that cover water treatment, bottle production, filling, capping, labeling, packaging, and logistics. This article outlines the key features you should evaluate when selecting a water filling machine and explains how a comprehensive solution provider can help you build a future-ready production line.
1. Integrated Blowing, Filling, and Capping System
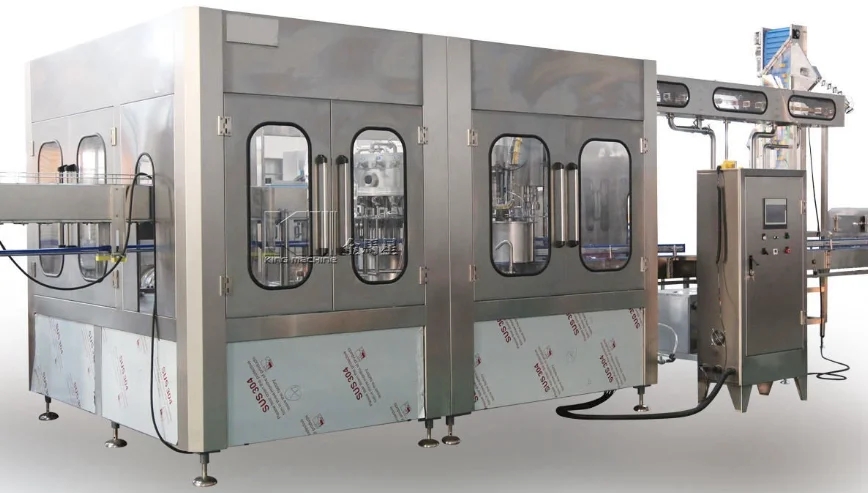
One of the most important developments in bottled water production is the integration of blowing, filling, and capping into a single system. A fully automatic three-in-one or blow-fill-cap machine significantly reduces:
-
Floor space requirements
-
Manual handling risks
-
Cross-contamination possibilities
-
Energy consumption
An integrated system ensures that PET preforms are blown into bottles and immediately transferred to the filling and sealing process in a controlled environment. This minimizes exposure to external contaminants and improves overall hygiene performance.
For producers focused on efficiency and sanitation, a fully automatic blow-fill-cap machine is now considered an industry standard rather than a luxury.
2. Hygienic Design and CIP Compatibility
Water may seem simple, but hygiene standards are extremely strict—especially for mineral water and purified drinking water. A high-quality water filling machine should feature:
-
Stainless steel 304/316 contact parts
-
Smooth, dead-angle-free internal surfaces
-
Hygienic valves and pipelines
-
Sealed filling environments
-
Compatibility with CIP (Clean-in-Place) systems
An integrated on-site automatic cleaning system ensures that production lines can be cleaned without disassembly. This not only improves sanitation but also reduces downtime and labor intensity.
When evaluating equipment, ask whether the system supports automated cleaning cycles and whether cleaning parameters can be recorded for traceability.
3. Precision Filling Technology
Accurate filling is critical for both regulatory compliance and brand reputation. Underfilling causes compliance issues; overfilling leads to product loss and increased costs.
Key filling technologies include:
-
Gravity filling (commonly used for water)
-
Negative pressure filling
-
Flow meter-based filling systems
Modern systems incorporate advanced flow control and sensor feedback to maintain consistent fill levels across high-speed production.
High-precision filling reduces material waste and improves overall line efficiency—particularly important for large-scale mineral water production lines.
4. Flexible Capacity and Bottle Compatibility
Production flexibility is a strategic advantage. A reliable water filling machine should support:
-
Multiple bottle sizes (small bottles to gallon containers)
-
Different cap types
-
Quick format changeovers
-
Adjustable production speeds
For manufacturers serving different markets, the ability to switch between 330ml, 500ml, 1.5L, or 5-gallon formats is essential. Changeover time directly affects productivity, so tool-free or fast-adjust systems are highly desirable.
5. Intelligent Control Systems
Modern beverage factories are moving toward smart workshop and smart factory models. A water filling machine should include:
-
PLC control systems
-
Human-machine interface (HMI) touchscreens
-
Real-time production monitoring
-
Alarm diagnostics
-
Data recording and export functions
Digital control improves traceability and simplifies troubleshooting. It also allows plant managers to analyze production data and optimize performance.
Companies investing in intelligent production lines gain better operational visibility and long-term scalability.
6. Energy Efficiency and Sustainability
Sustainability is no longer optional. Energy-efficient motors, optimized air consumption in blowing systems, and water-saving cleaning processes all contribute to lower operational costs and reduced environmental impact.
Features to look for:
-
High-efficiency servo motors
-
Optimized compressed air usage
-
Heat recovery systems
-
Reduced wastewater discharge
A well-designed system reduces overall resource consumption while maintaining high output levels.
7. Complete Turnkey Solution Capability
Many manufacturers face challenges when sourcing different equipment from multiple suppliers. Compatibility issues, installation delays, and inconsistent after-sales service can slow down project implementation.
Working with a company that offers a complete solution—from water treatment to secondary packaging—ensures smooth integration and unified technical standards.
8. Water Treatment System Integration
A filling machine is only as good as the water quality feeding into it. A complete mineral water or purified water line should include:
-
Multi-stage filtration
-
Reverse osmosis systems
-
UV sterilization
-
Ozone treatment
-
Sterilization equipment sets
Integrated water treatment ensures consistent product quality and compliance with local drinking water standards.
9. Labeling, Conveying, and Secondary Packaging
A filling machine is one part of a broader production chain. To achieve stable and efficient output, the following supporting systems must be seamlessly integrated:
-
Automatic labeling systems
-
Bottle conveying systems
-
Shrink wrapping or carton packaging
-
Palletizing solutions
Coordinated line control ensures that bottlenecks are minimized and throughput remains consistent.
10. Proven Experience and Certifications
When investing in high-value industrial equipment, supplier credibility matters. Look for manufacturers that:
-
Hold ISO9000 quality management certification
-
Have recognized high-tech enterprise credentials
-
Possess in-house R&D and manufacturing capabilities
-
Have proven export experience
A company with over 20 years of experience in beverage packaging machinery demonstrates both technical maturity and market validation.
Case Insight: Comprehensive Beverage Packaging Expertise
A comprehensive manufacturer based in Shenzhen, China, located in Bao’an District Songgang Street, integrates research, development, and production of beverage packaging machinery. Over two decades, the company has continuously introduced and improved global beverage packaging technologies under the philosophy of “introduction and improvement, technological advancement.”
Its core product portfolio includes:
-
Fully automatic blow molding machines
-
Blow-fill-cap integrated production lines
-
Gallon barrel production lines
-
Water treatment production lines
-
On-site automatic cleaning systems
-
Sterilization equipment
-
Bottled filling and sealing lines
-
Complete juice and carbonated beverage production lines
-
Intelligent cleaning systems and industrial cleaning solutions
By covering every stage—from procurement and production to packaging, warehousing, logistics, and distribution—the company supports customers in building fully integrated beverage factories.
Its products are sold in over 20 provinces domestically and exported to countries including the UAE, Oman, Vietnam, the Philippines, and Malaysia, earning strong market recognition.
11. After-Sales Service and Technical Support
Even the most advanced equipment requires reliable support. Before selecting a supplier, evaluate:
-
Installation and commissioning services
-
Operator training programs
-
Spare parts availability
-
Remote technical assistance
-
Long-term maintenance support
A supplier that provides comprehensive service ensures minimal downtime and protects your investment over the equipment lifecycle.
Final Thoughts
A water filling machine is not just a piece of equipment—it is the core of your beverage production operation. When evaluating options, look beyond basic specifications. Focus on:
-
Integration capabilities
-
Hygiene and sanitation design
-
Intelligent control systems
-
Production flexibility
-
Energy efficiency
-
Full-line compatibility
Selecting a reliable, experienced manufacturer with complete beverage packaging expertise allows you to build a stable, scalable, and competitive production facility.
As global demand for safe drinking water continues to grow, investing in advanced, intelligent filling systems is not only a technical decision—it is a strategic one.