

The carbonated soft drink industry has experienced significant changes over the past decades. As consumer demand grows for consistent taste, safe packaging, and faster delivery, beverage manufacturers are under increasing pressure to improve production efficiency while maintaining strict quality standards. Traditional manual operations are gradually being replaced by automated systems that provide better control over filling accuracy, hygiene management, and production stability.
Automation is no longer limited to individual machines. Modern carbonated soft drink production lines integrate water treatment, beverage preparation, filling, capping, labeling, inspection, conveying, and packaging into a complete intelligent manufacturing system. These integrated solutions help beverage producers reduce operational risks and achieve higher production efficiency.
As a professional beverage packaging machinery manufacturer, Pengxiang Huixing provides comprehensive solutions covering water treatment systems, beverage pre-treatment systems, PET blowing equipment, blow-fill-seal production lines, blow-label-fill-seal systems, labeling machines, conveyor systems, and secondary packaging equipment. The company focuses on intelligent workshop planning, smart factory design, and advanced liquid beverage packaging technologies to support customers throughout the entire production process.
The Growing Need for Automation in Carbonated Beverage Production
Carbonated soft drink manufacturing involves multiple sensitive processes, including water purification, ingredient mixing, carbonation, temperature control, filling, and sealing. Any small variation during production can affect product quality.
For example, incorrect filling pressure may cause excessive foaming, while unstable carbonation levels can change the taste experience. Manual adjustments are often time-consuming and difficult to maintain consistently during long production cycles.
Automation addresses these challenges by using advanced control systems, sensors, and intelligent equipment to monitor production conditions in real time. Automated filling systems can maintain stable pressure, precise volume control, and consistent product quality even during high-speed operations.
Modern beverage factories are increasingly adopting automated production lines because they provide:
-
Higher production consistency
-
Reduced dependence on manual operation
-
Improved hygiene control
-
Better production data management
-
More efficient resource utilization
These advantages are particularly important for large-scale carbonated soft drink manufacturers that need reliable production performance.
Intelligent Filling Technology Improves Production Accuracy
The filling process is one of the most important stages in carbonated soft drink production. Unlike still beverages, carbonated drinks require precise control of pressure and temperature to prevent carbonation loss and excessive foaming.
Automated filling machines use advanced control technology to manage filling speed, pressure balance, and liquid levels. The system can automatically adjust operating parameters according to production conditions, ensuring every bottle receives the correct amount of beverage.
Modern filling equipment also integrates automatic cleaning and sterilization functions. These technologies help reduce contamination risks and improve production safety.
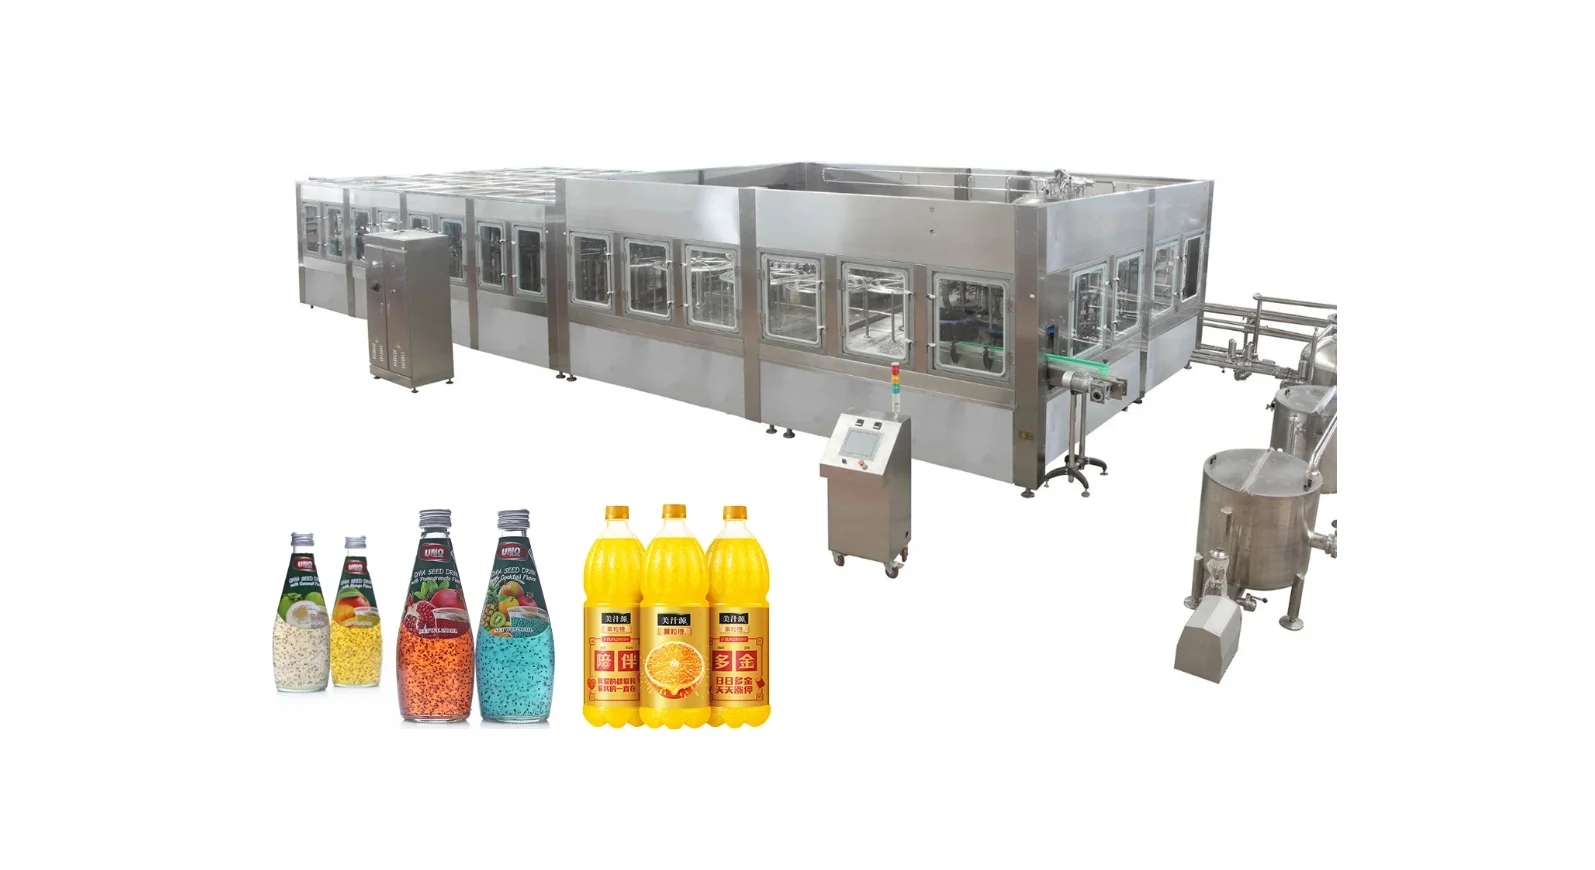
Pengxiang Huixing develops and manufactures advanced beverage filling solutions, including complete carbonated beverage production systems. Its equipment supports manufacturers with integrated technologies from beverage processing to final packaging, helping customers build efficient and stable production environments.
For companies looking for specialized carbonated beverage filling solutions, Pengxiang Huixing provides complete systems :
These systems are designed to meet the requirements of modern beverage factories, combining automation, reliability, and production flexibility.
Automation Creates Smarter Beverage Production Lines
The development of Industry 4.0 has accelerated the transformation of beverage factories. Smart production lines are now equipped with digital monitoring systems, automated control platforms, and data collection technologies.
A smart carbonated soft drink production line can monitor:
-
Equipment operating status
-
Production speed
-
Filling accuracy
-
Energy consumption
-
Cleaning procedures
-
Maintenance requirements
Through centralized control systems, operators can quickly identify potential issues and optimize production performance. Instead of relying only on manual inspections, manufacturers can use real-time data analysis to make better production decisions.
Pengxiang Huixing specializes in intelligent workshop and smart factory planning, helping beverage companies create complete production solutions. From raw water treatment to finished product packaging, the company provides equipment and technical services covering procurement, manufacturing, packaging, storage, logistics, and distribution.
The Role of Automation in Hygiene and Safety Control
Food and beverage safety is a major concern for manufacturers worldwide. Carbonated soft drinks require strict hygiene management throughout the entire production process.
Automated systems help improve sanitation by reducing unnecessary human contact with production materials. Closed production environments, automated cleaning systems, and precise process control significantly reduce contamination risks.
For example, automated Clean-In-Place (CIP) systems can clean pipelines, tanks, and filling equipment without requiring extensive manual disassembly. This not only improves cleaning efficiency but also ensures more consistent sanitation results.
Pengxiang Huixing provides intelligent cleaning systems, industrial cleaning solutions, and automatic cleaning equipment designed for beverage production facilities. These solutions help manufacturers maintain stable hygiene standards while improving production efficiency.
Automation Enhances Energy and Resource Efficiency
Sustainable manufacturing has become an important goal for beverage companies. Automated production equipment helps reduce waste and optimize the use of water, electricity, and raw materials.
Advanced filling systems can minimize product loss by improving filling precision. Intelligent control systems can adjust equipment operation based on actual production needs, reducing unnecessary energy consumption.
Water treatment systems also play an important role in efficient beverage production. High-quality treated water is essential for carbonated beverages because water quality directly influences product taste and stability.
Pengxiang Huixing provides complete water treatment production lines and beverage pre-processing systems that support manufacturers in producing high-quality beverages with reliable water management.
Automation Supports Flexible Beverage Manufacturing
Consumer preferences continue to change, and beverage companies need flexible production capabilities. Different markets require various bottle sizes, packaging formats, and beverage categories.
Automated production lines allow manufacturers to switch production parameters more efficiently. Equipment such as PET blowing machines, filling systems, labeling machines, and conveyor systems can be integrated to support multiple product formats.
This flexibility enables beverage producers to respond quickly to market demands while maintaining production efficiency.
Pengxiang Huixing offers complete beverage packaging machinery solutions, including PET blowing equipment, filling and capping production lines, labeling systems, conveyor systems, and secondary packaging equipment. These integrated solutions help customers improve production flexibility and build competitive manufacturing systems.
The Future Development of Automated Carbonated Soft Drink Production
Automation in the beverage industry will continue to develop with advances in artificial intelligence, digital management, and intelligent manufacturing technologies.
Future carbonated soft drink factories are expected to become more connected, with equipment communicating through digital platforms and production data being analyzed automatically. Predictive maintenance systems will help reduce unexpected downtime, while intelligent control systems will further improve production efficiency.
Manufacturers that invest in automation will have stronger capabilities in quality management, production optimization, and market response.
With more than 20 years of experience in beverage packaging machinery technology, Pengxiang Huixing has continuously improved its solutions through technology introduction and innovation. The company has developed unique market advantages by combining global beverage machinery technologies with continuous improvement.
Located in Songgang Street, Bao'an District, Shenzhen, China, Pengxiang Huixing is a comprehensive beverage packaging machinery manufacturer integrating research, development, and production. Its products have passed ISO9000 quality management system certification and the company has been recognized as a China High-Tech Enterprise.
Its solutions are widely used in domestic markets and exported to countries and regions including the United Arab Emirates, Oman, Vietnam, the Philippines, and Malaysia.
Conclusion
Automation is reshaping carbonated soft drink filling processes by improving accuracy, efficiency, hygiene, and production flexibility. From intelligent filling machines to complete smart factory solutions, automated technologies are helping beverage manufacturers meet modern market requirements.
Companies that adopt integrated automation solutions can achieve more stable production, better quality control, and stronger long-term competitiveness.
As beverage production continues to move toward intelligent manufacturing, advanced machinery suppliers like Pengxiang Huixing will continue to support global customers with complete beverage processing and packaging solutions, helping build efficient and reliable beverage factories for the future.