

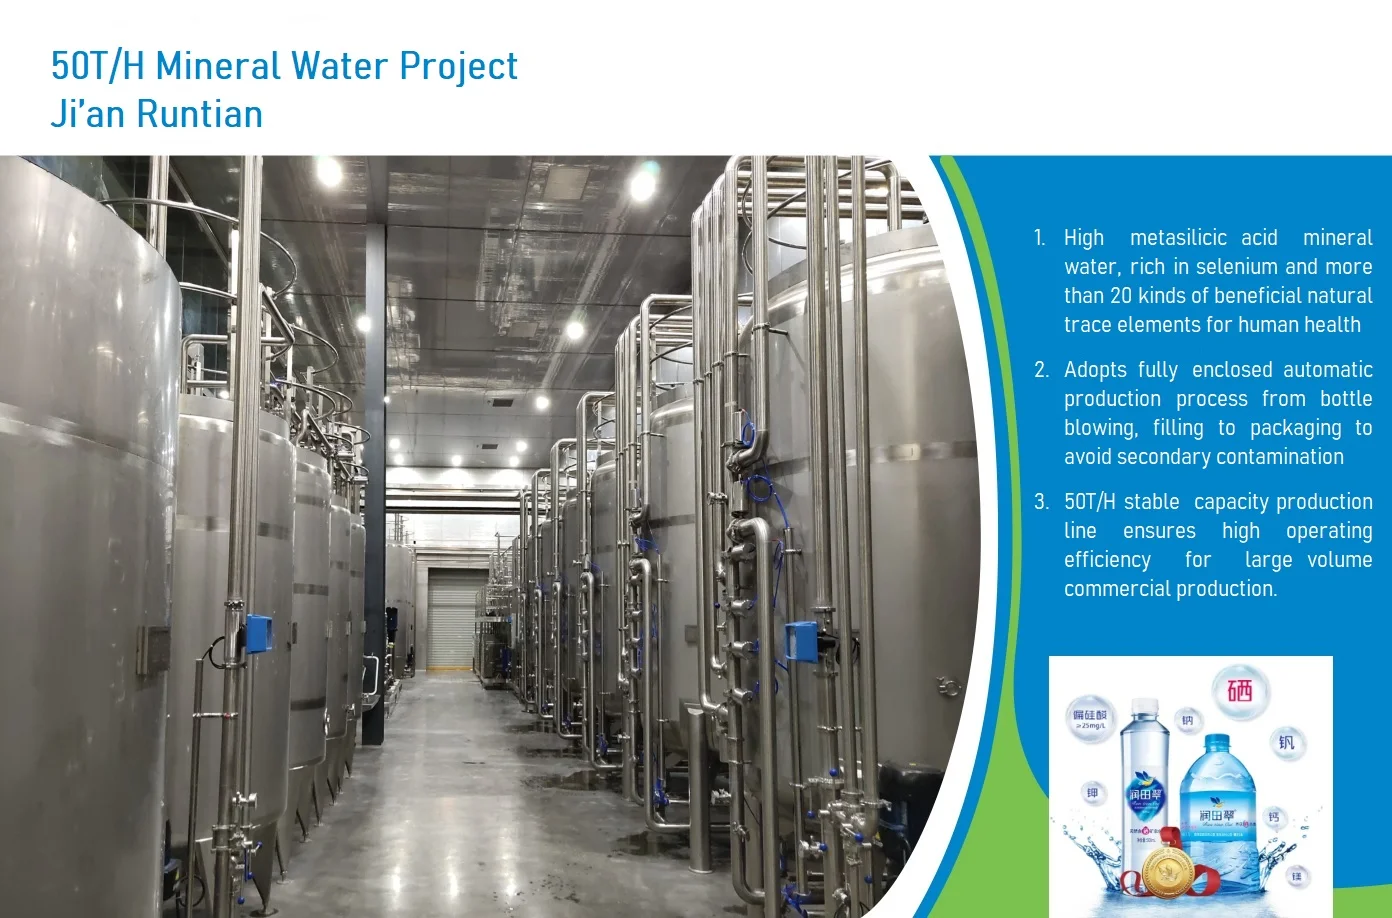
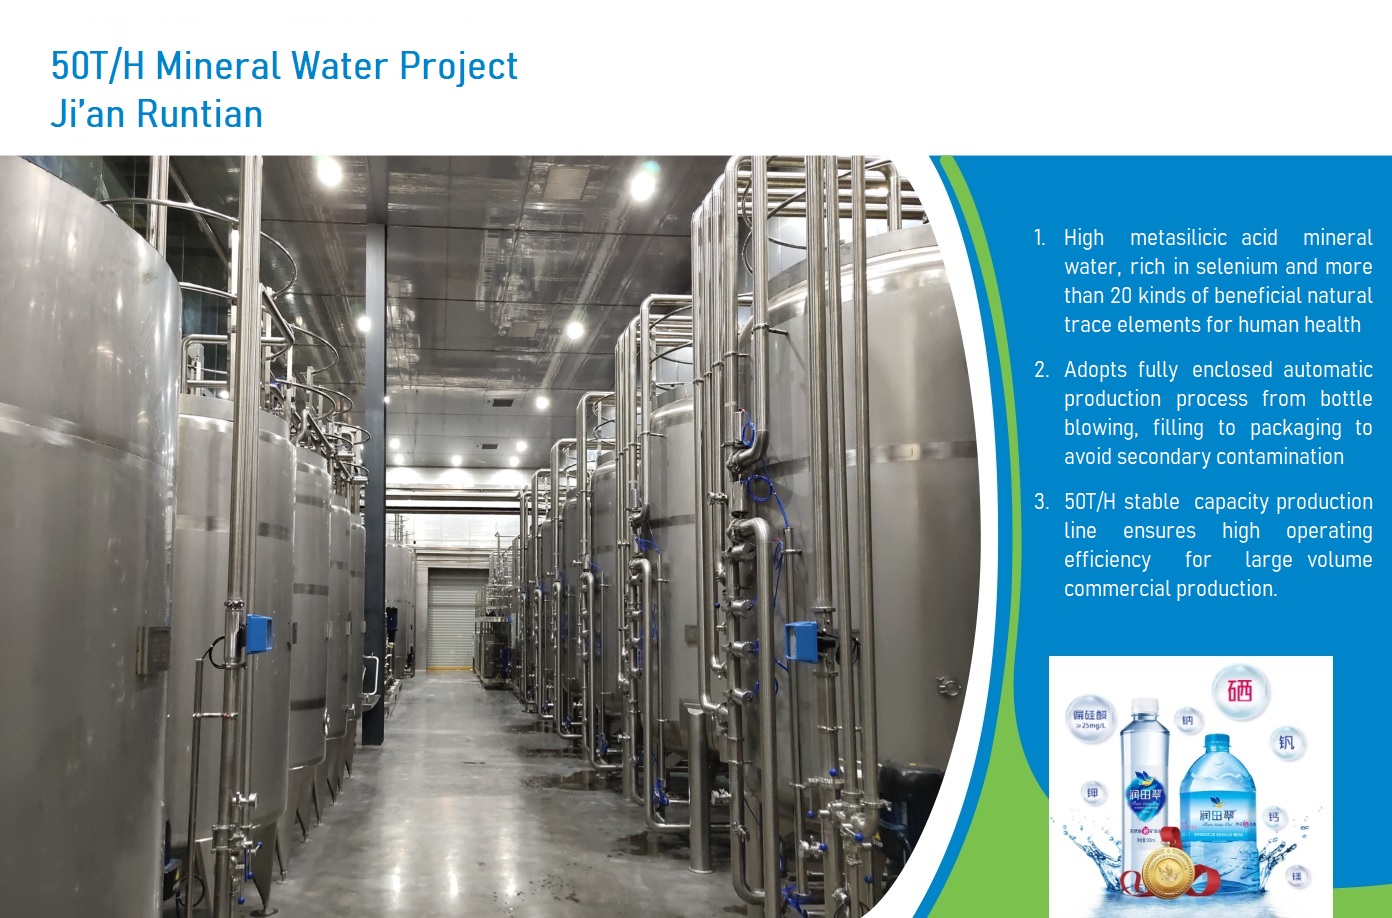
50 T/H
Jiangxi Runtian Beverage
A Sino-foreign joint venture founded in 1994, producing natural beverage products under a brand positioning built around returning to nature and paying attention to health.
The Jiangxi Runtian 50L/hour mineral water production project represents a benchmark high-end natural mineral water manufacturing project in China’s beverage industry. Rooted in the world-famous selenium-rich water source of Mingyue Mountain, Yichun, the project focuses on the production of high-quality natural selenium-rich mineral water, which is rich in natural selenium, metasilicic acid and various trace elements beneficial to the human body, with natural weak alkalinity and fresh and sweet taste. As the exclusive turnkey equipment and engineering service provider for this project, we delivered customized water treatment systems, full-automatic filling production lines and standardized whole-plant layout & commissioning services, creating a highly efficient, stable and hygienic modern mineral water production base for Runtian.
Project Core Advantages & Water Source Features
Different from ordinary purified water production, this project targets premium natural mineral water with rare ecological water source advantages. The raw water is taken from deep underground ancient aquifers of Mingyue Mountain, a reputed “World Selenium Health Capital”, featuring zero industrial pollution, stable water quality and rich natural active trace elements. To completely retain the natural mineral activity and nutritional value of raw water while meeting commercial sterility and long-shelf-life requirements, the project adopts a scientific low-loss purification and sterile filling process, avoiding excessive treatment that damages natural water quality.
With a stable capacity 50L/H, the production line realizes continuous and standardized mass production of high-end selenium-rich mineral water. It fully meets the market demand for high-quality bottled drinking water for daily consumption, business reception, sports and travel, and supports long-term brand market expansion and export certification standards.
Our Customized Water Treatment System Advantages for Mineral Water
Ordinary RO pure water treatment equipment will remove all natural minerals and trace elements, failing to meet mineral water production standards. For the unique water quality characteristics of Runtian selenium-rich mineral water, we designed a specialized graded low-interference purification system, which is the core guarantee of the project’s product quality.
The system adopts multi-stage precision filtration and selective purification technology, which effectively intercepts suspended solids, colloids, bacteria and organic impurities in raw water. Meanwhile, it completely retains beneficial minerals such as selenium and metasilicic acid unique to the water source, perfectly balancing water safety and natural mineral activity. Compared with conventional single-process equipment, our customized mineral water treatment solution features low water quality loss, stable water output parameters and strong anti-fluctuation ability, adapting to seasonal tiny changes of natural source water to ensure consistent taste and quality of each batch of products.
In addition, the whole water treatment system adopts food-grade sanitary stainless steel pipeline and dead-corner-free design, matched with automatic CIP cleaning circulation system, which effectively prevents secondary pollution, fully complies with food GMP production specifications, and meets the strict quality inspection standards of high-end mineral water.
Full-Automatic Whole-Line Production Configuration Strength
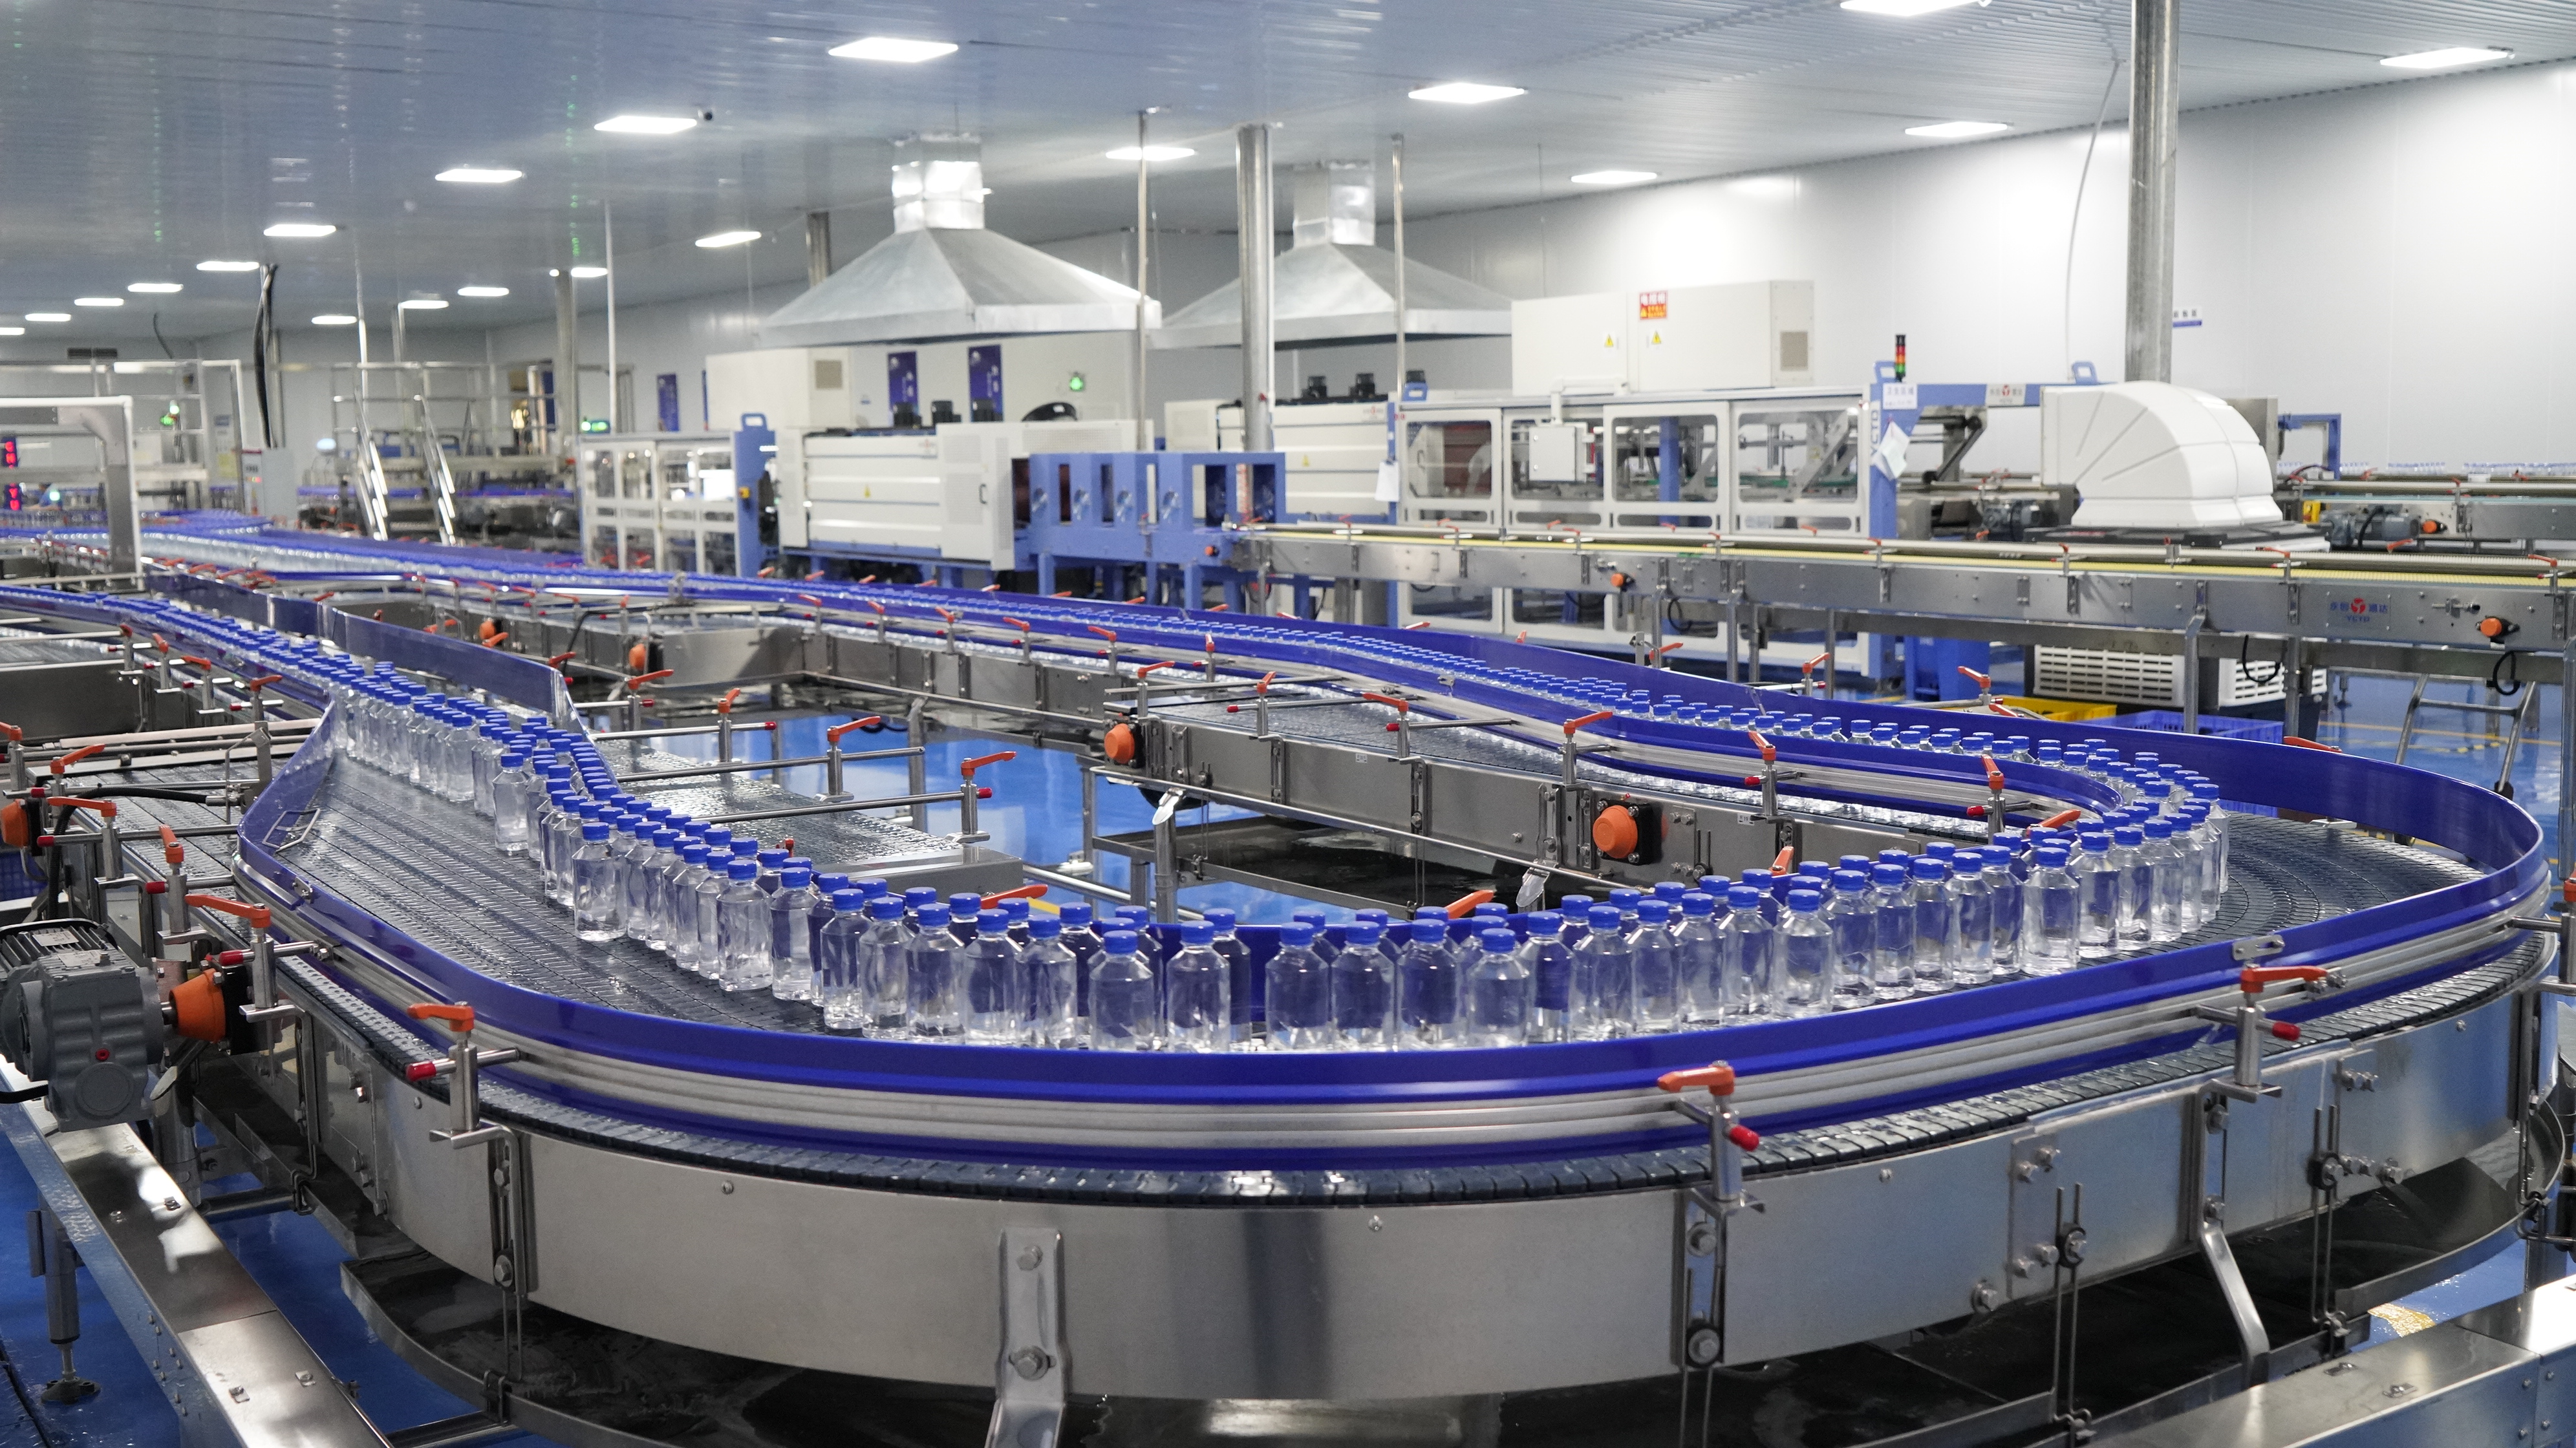
We provide a complete integrated production solution from water treatment, bottle blowing, rinsing-filling-capping integration, labeling, coding to automatic cartoning for the Runtian project. The whole line realizes fully automated unmanned operation with synchronized and stable rhythm.
The core 3-in-1 filling machine adopts mineral water-specific constant-pressure sterile filling technology, with accurate liquid level control, no overflow and no leakage. It effectively protects the natural activity of mineral water and avoids secondary bacterial contamination. The supporting high-speed labeling system and intelligent packaging equipment are perfectly matched with the main line speed, eliminating production bottlenecks and maximizing the 50L/ rated production capacity.
Our Professional Engineering & Customization Capabilities
1. Water Quality-Oriented Customized Process Design We abandon standardized general equipment schemes. According to the unique indicators of Runtian selenium-rich mineral water source, we conduct targeted process deduction and equipment configuration, ensuring that the treatment process is neither excessive nor insufficient, precisely retaining the core competitive advantages of natural mineral water.
2. Scientific Whole-Plant Layout & Standardized Installation We provide professional CAD construction drawings and 3D workshop layout simulation, reasonably dividing raw water treatment area, sterile filling purification area, finished product storage area and logistics channel. The optimized process layout shortens the material conveying path, improves production efficiency, and reserves sufficient operation and maintenance space. All installation and wiring are implemented in strict accordance with national food safety standards and project certification requirements.
3. Strict Pre-Delivery Debugging & On-Site Commissioning All core equipment undergoes full-load linkage debugging before leaving the factory. Professional engineers conduct on-site assembly, whole-line synchronous calibration, parameter optimization and trial production guidance to ensure the stable output of the 50L/min standard capacity and qualified product yield rate.
4. Full-Lifecycle Technical After-Sales Support We provide 12-month full machine warranty, 24-hour remote fault troubleshooting, regular preventive maintenance and original spare parts supply. Long-term technical follow-up ensures the long-term stable, low-consumption and high-efficiency operation of the entire mineral water production line.
Project Summary
The successful operation of Jiangxi Runtian 50L/Hour mineral water project fully verifies our professional strength in customized design, whole-line supporting configuration, standardized installation and commissioning for high-end natural mineral water projects. We accurately solve the industry pain points of difficult retention of natural mineral elements and unstable water quality in mineral water production. With mature turnkey project experience, we provide reliable, high-standard and cost-effective integrated solutions for global high-quality mineral water production enterprises.
Project Gallery
Site photographs from installation through to commissioning.
More Projects
All ProjectsOther Mineral Water Systems
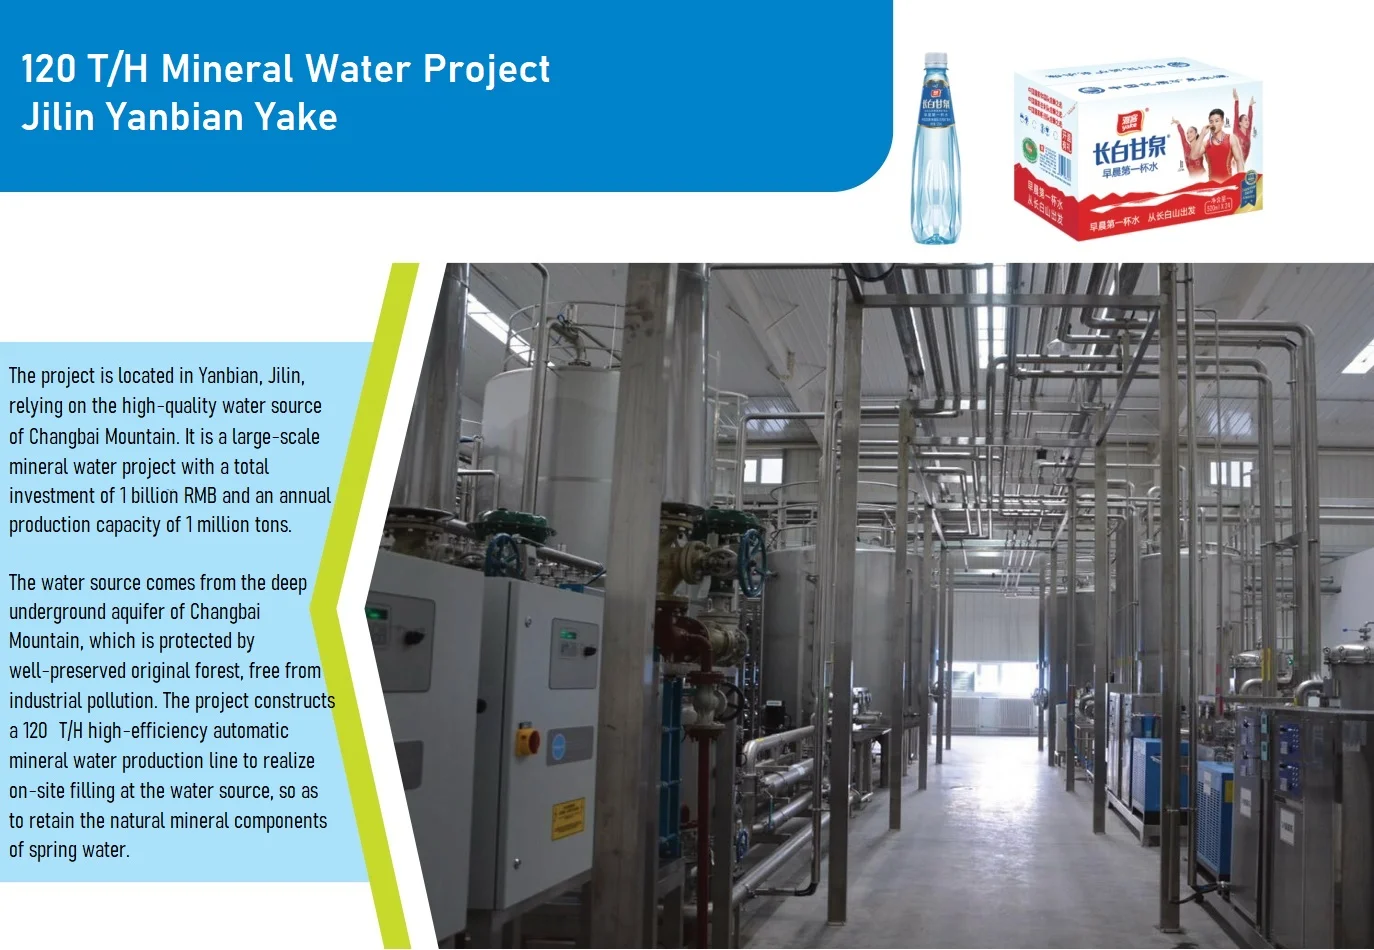
120 T/H Yanbian Yake Changbai Mountain Mineral Spring
Antu County, Jilin. A 1-billion-RMB plant with 1 million tonnes annual capacity, in China's mineral water hear...
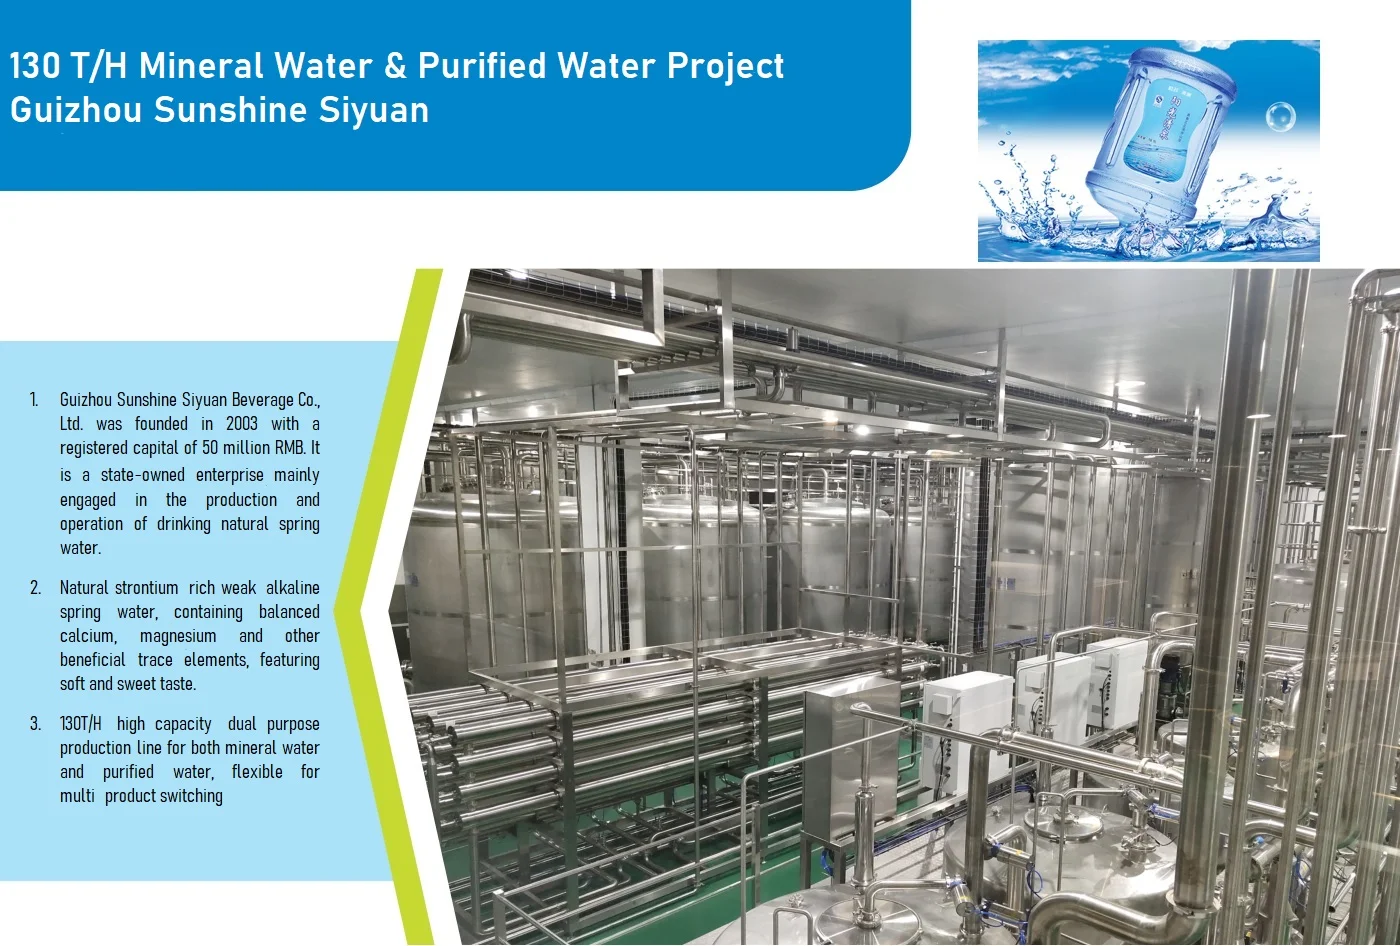
130 T/H Guizhou Sunshine Siyuan Drink
State-owned producer founded in 2003, running combined mineral and purified water production.
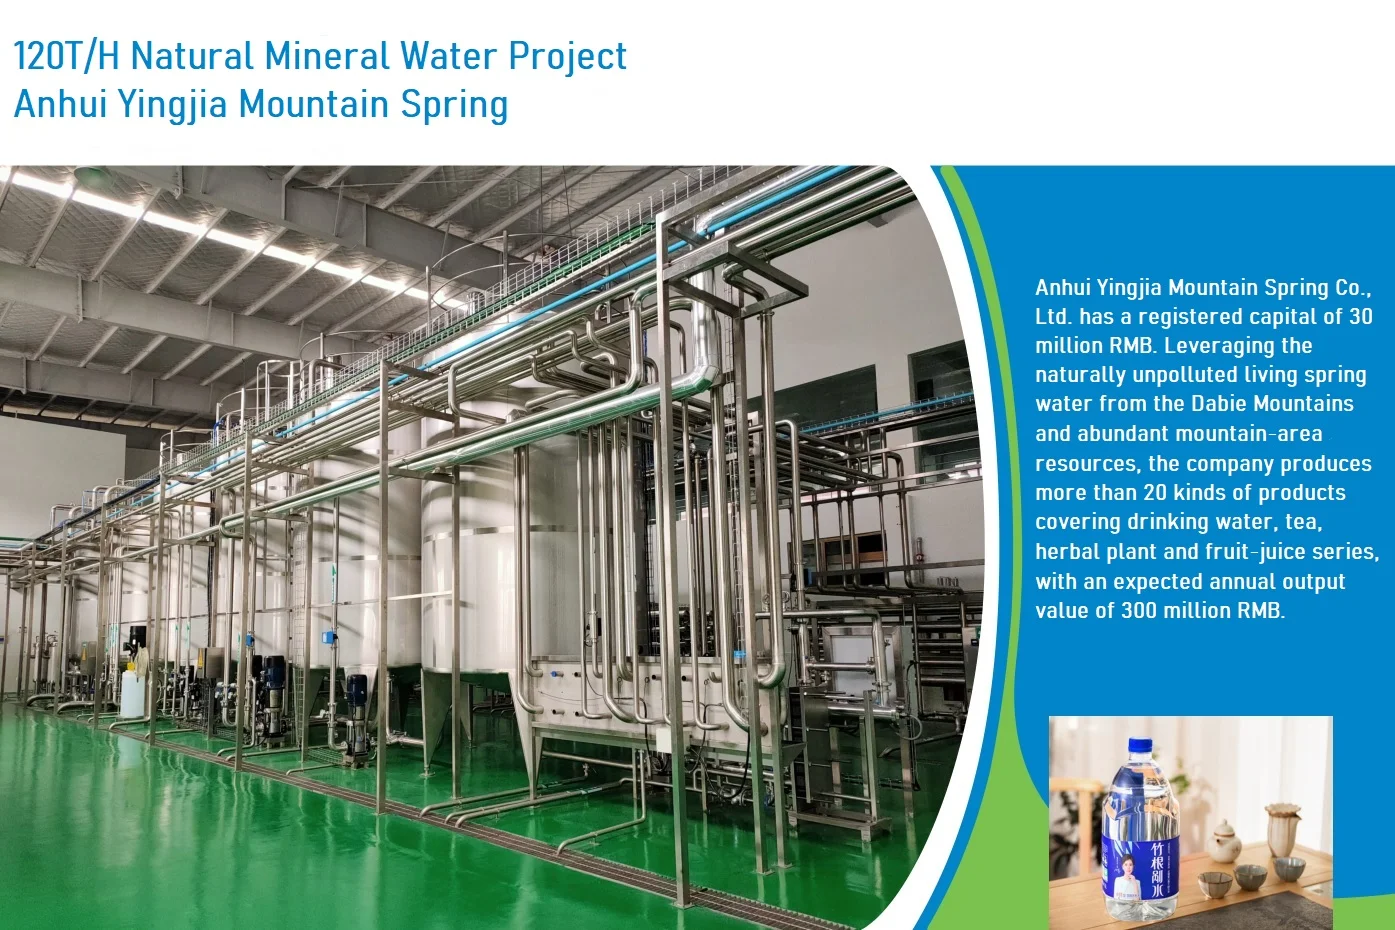
120 T/H Anhui Yingjia Mountain Spring
A 120 tonnes per hour mineral water treatment system for a Dabie Mountain spring source, supporting a plant th...