

50 T/H
Kunming Jingming Food — Zhenming, Songming
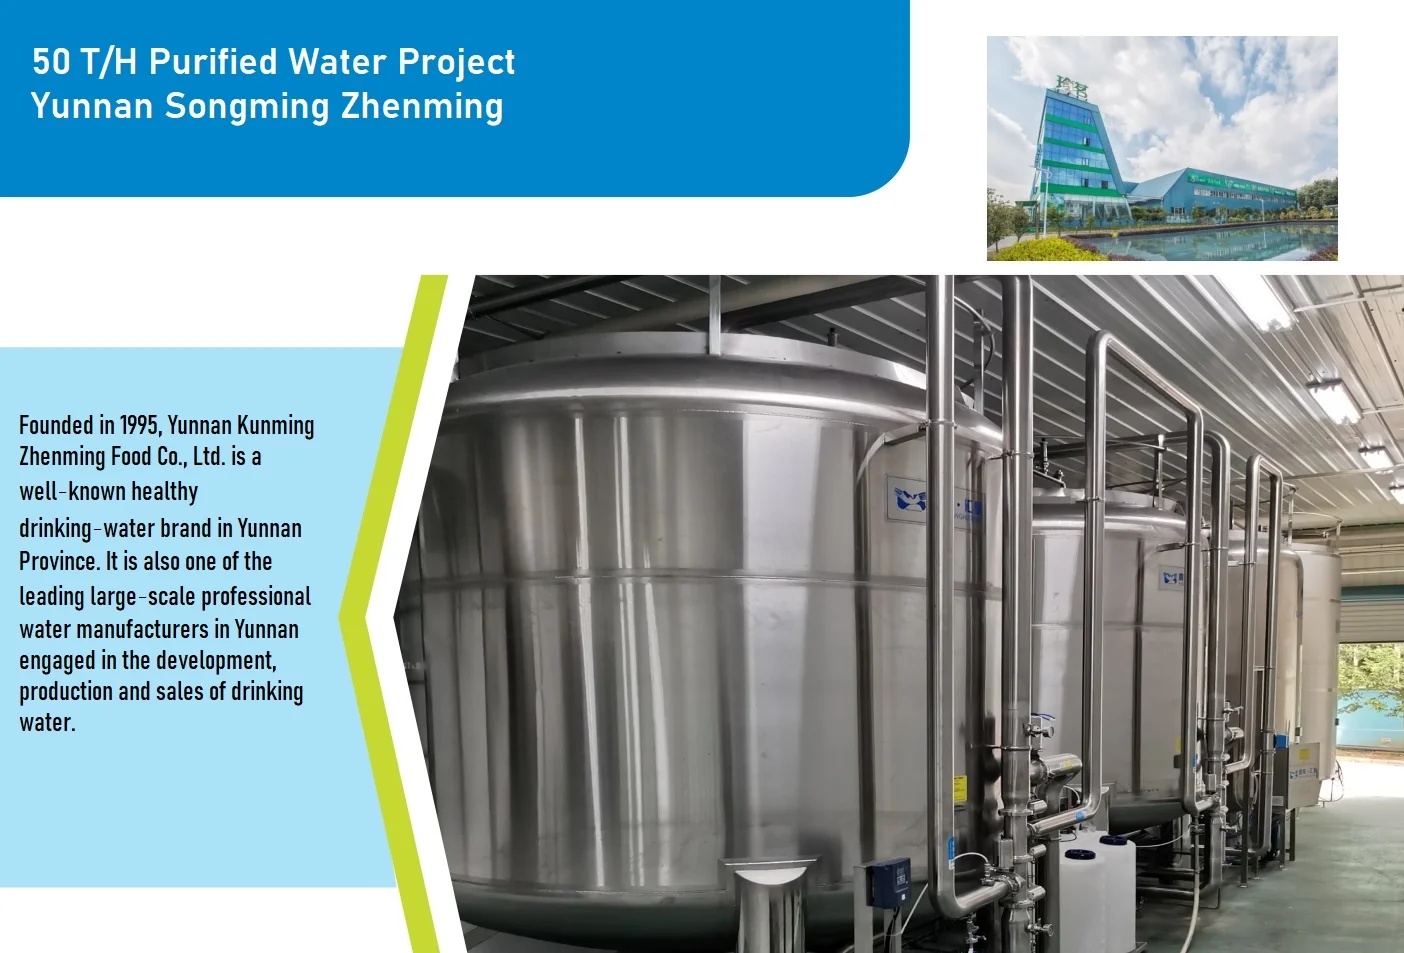
Founded in 1995 and one of Yunnan Province's best-known healthy drinking water brands, ranked among the province's leading enterprises in drinking water development, production and sales.
The Kunming Zhenming 50-ton/hour purified water production line is a benchmark intelligent and green water manufacturing project in Yunnan, China. As a leading local drinking water brand with a national green factory certification, Zhenming focuses on high-standard purified water production with strict food safety and stable water quality requirements. We delivered the full-turnkey solution for this project, covering customized water treatment system, automatic filling line, complete plant layout design, standardized installation and full-line commissioning. The project realizes continuous, high-efficiency and low-consumption purified water mass production, representing our mature engineering strength in large-scale water beverage factory construction.
Project Overview & Core Operational Advantages
Designed with a stable capacity of 50 tons per hour, the production line meets large-volume, 24-hour continuous commercial production for bottled and barreled purified water. Built in strict accordance with GMP food-grade workshop standards and national green factory specifications, the whole production process adopts closed and sterile operation modes. Supported by a complete full-process quality control system and one-code traceability management, the project achieves zero secondary pollution, stable water quality indicators and consistent batch quality, fully complying with domestic and international drinking water safety standards.
Different from ordinary small and medium-sized water lines, this customized high-capacity production line features intelligent operation, low operating cost and high resource utilization rate. It perfectly matches Zhenming’s large-scale production layout and long-term brand quality upgrading strategy.
Our Professional Water Treatment System Advantages
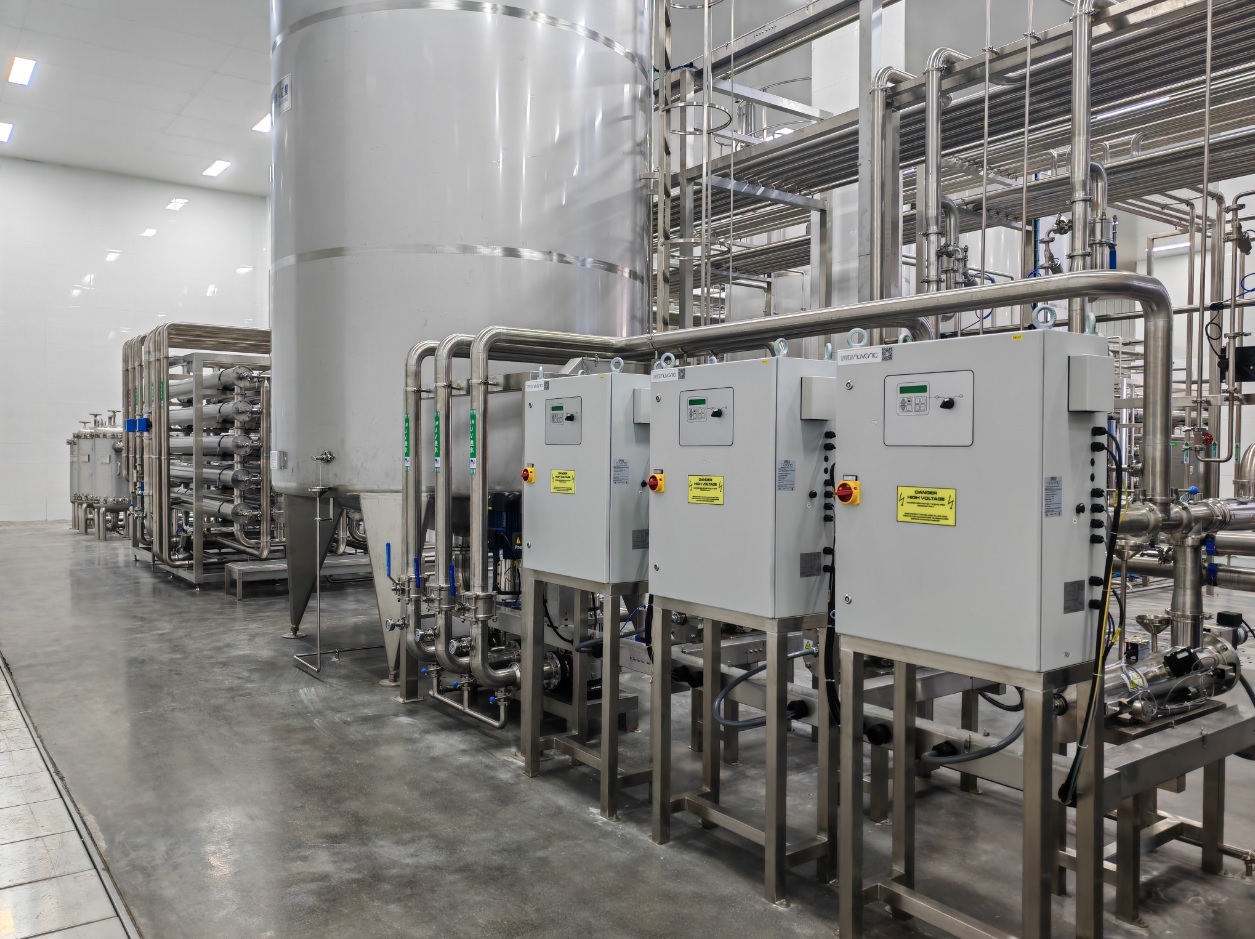
Aiming at the local raw water characteristics of Kunming area, we designed a multi-stage graded purification RO water treatment system exclusively for this project. The equipment adopts precision mechanical filtration, activated carbon adsorption, softening treatment and double-stage reverse osmosis technology, effectively removing suspended solids, colloid, excess ions, heavy metals and microorganisms in raw water. The treated water features stable TDS value, low hardness and high purity, fully reaching qualified purified water drinking standards.
To adapt to 50T/h high-load continuous operation, we optimized the system water flux and membrane anti-fouling performance. The enhanced anti-clogging structure and automatic flushing program greatly extend the service life of filter membranes and reduce daily maintenance frequency. Compared with conventional water treatment equipment, our customized system saves more than 25% of water and electricity consumption, realizing energy-saving and environmentally friendly green production.
Full-Automatic Whole-Line Configuration Strength
We equipped the project with a fully integrated intelligent production line, covering automatic bottle blowing, high-speed rinsing-filling-capping 3-in-1 machine, precise labeling, coding, film wrapping and automatic palletizing systems. The whole line achieves unmanned synchronous linkage operation from raw water inflow to finished product outbound.
The core filling host adopts constant-pressure gravity filling technology, ensuring accurate liquid level, no overflow and no leakage. The food-grade full sanitary pipeline design without dead corners supports automatic CIP cleaning, effectively avoiding material residue and bacterial growth. The matched high-speed rear-end packaging equipment maintains consistent line speed, completely eliminating production bottlenecks and maximizing the 50T/h rated production capacity.
Our Customized Design, Installation & Engineering Capabilities
1. Site-Adapted Scientific Layout Design According to the customer’s factory area, workshop structure and green factory construction standards, we completed professional CAD layout and 3D simulation planning. We reasonably divided the water treatment area, sterile filling purification area, packaging area and finished product storage area, optimizing production logistics routes and saving workshop space. The standardized zoning design meets GMP purification requirements and national green factory audit standards.
2. High-Capacity Whole-Line Synchronization Debugging Facing the high matching difficulty of 50T/h large-capacity equipment, we unified the operating rhythm of front and rear equipment through pre-delivery FAT full-linkage testing and on-site precise calibration. All electrical signals, operating frequency and transmission speed are accurately matched to ensure stable and continuous operation of the whole line without jamming, shutdown or speed mismatch.
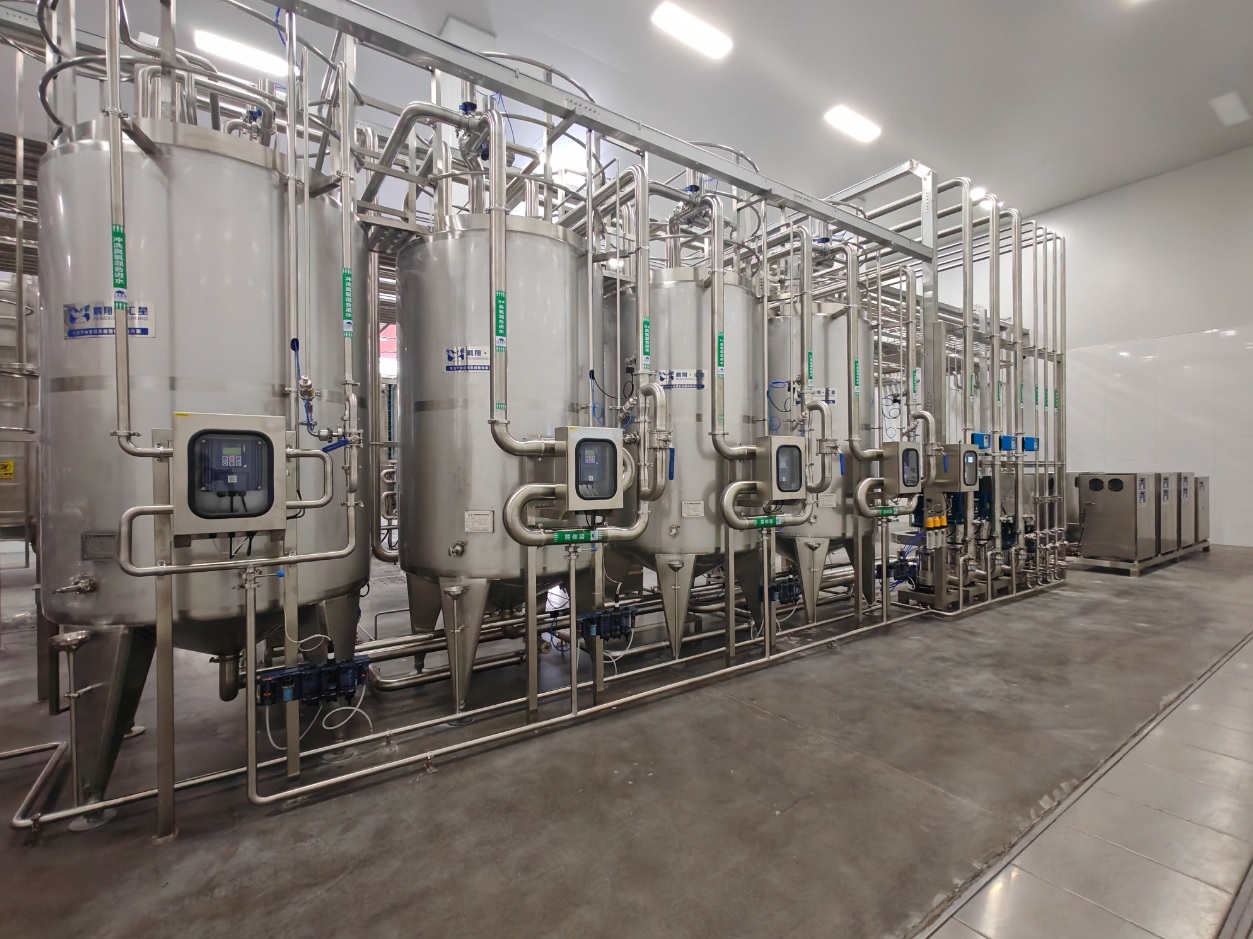
3. Strict Sanitary & Quality Control System All wetted parts adopt food-grade 304/316 stainless steel and high-purity sanitary accessories. We configured multi-channel online water quality monitoring devices to realize real-time early warning of water quality abnormalities. Combined with the customer’s one-code traceability system, we build a double quality guarantee mechanism for equipment process and production management.
4. Full-Cycle Turnkey Service Guarantee We provided one-stop services including project scheme design, equipment manufacturing, factory layout guidance, on-site installation, whole-line commissioning and operator training. After project delivery, we offer long-term remote technical support, regular preventive maintenance and original spare parts supply, ensuring the long-term stable and low-failure operation of the large-capacity production line.
Project Value & Summary
The successful operation of the Kunming Zhenming 50-ton/hour purified water project fully demonstrates our outstanding capabilities in large-capacity water line customization, intelligent whole-line matching, standardized installation and green process optimization. We solve the industry pain points of unstable water quality, high energy consumption and difficult linkage debugging for large-scale purified water production. With reliable technical strength and mature turnkey project experience, we continue to provide high-standard, energy-saving and intelligent overall solutions for global purified water and beverage factory projects.
Project Gallery
Site photographs from installation through to commissioning.
More Projects
All ProjectsOther Mineral Water Systems
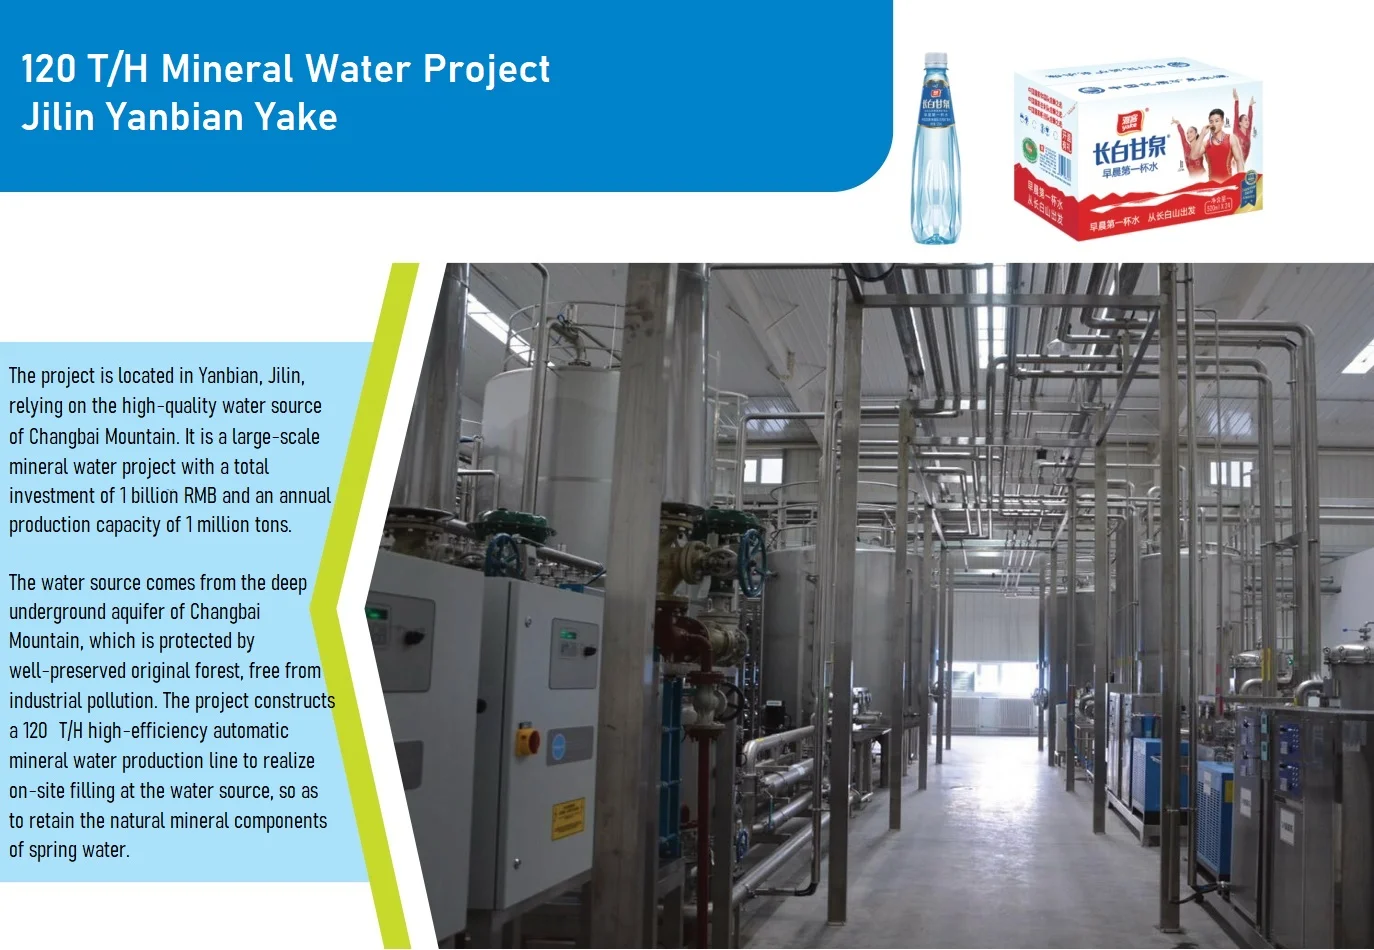
120 T/H Yanbian Yake Changbai Mountain Mineral Spring
Antu County, Jilin. A 1-billion-RMB plant with 1 million tonnes annual capacity, in China's mineral water hear...
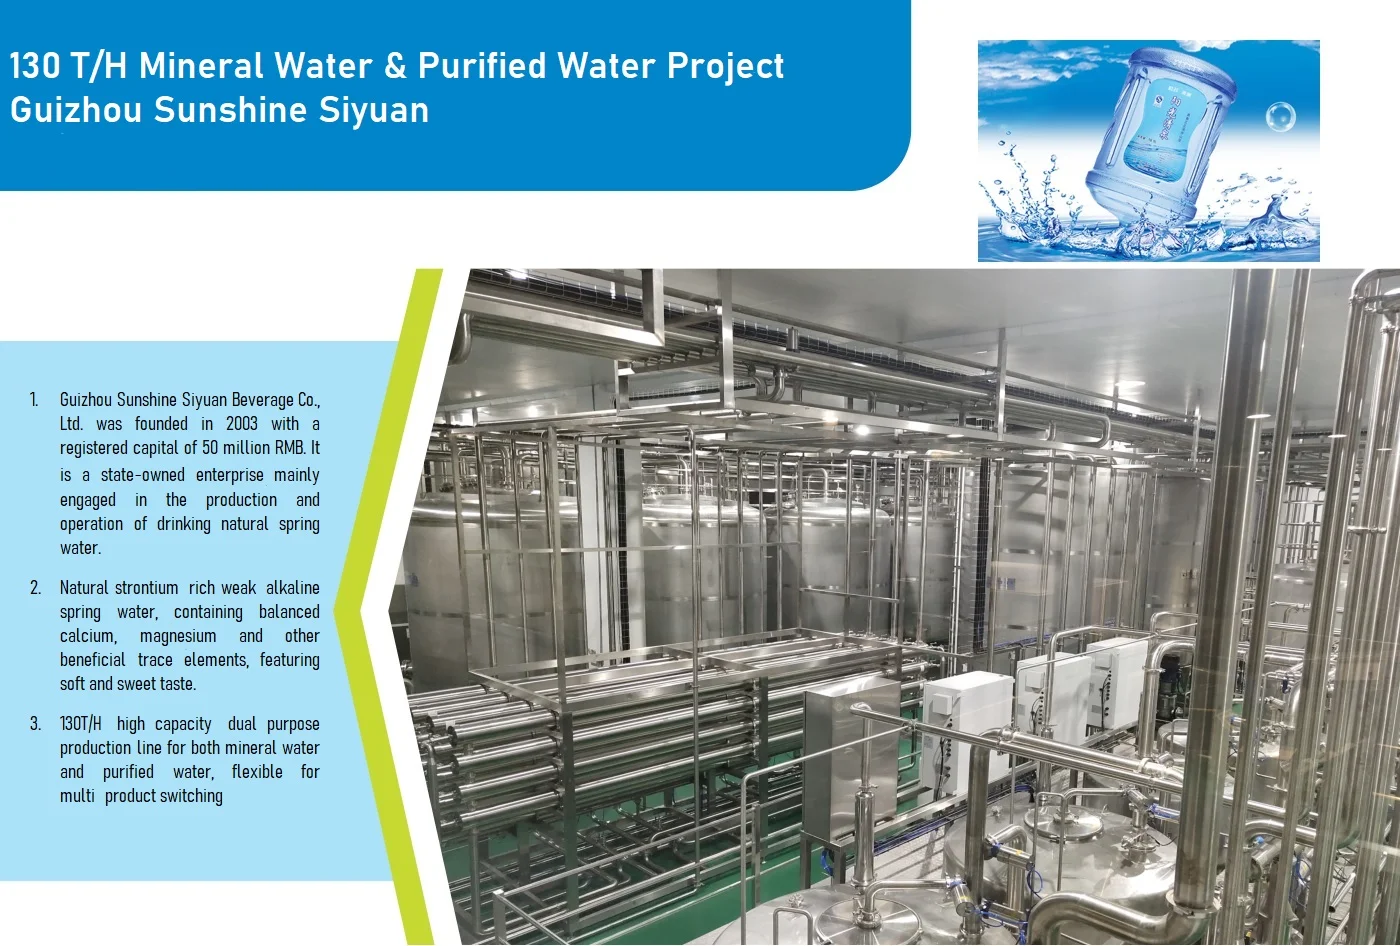
130 T/H Guizhou Sunshine Siyuan Drink
State-owned producer founded in 2003, running combined mineral and purified water production.
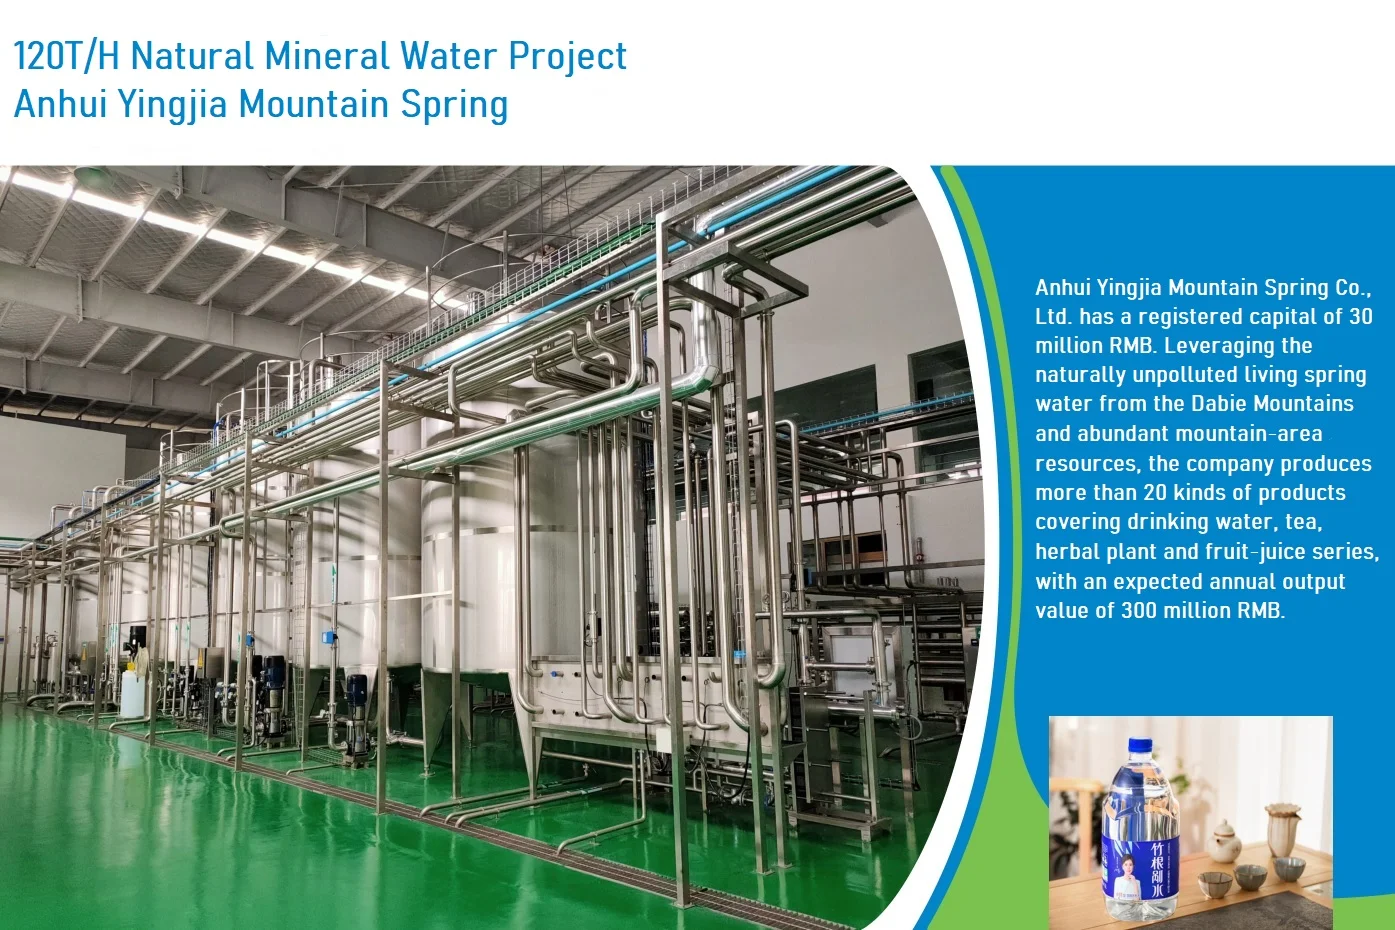
120 T/H Anhui Yingjia Mountain Spring
A 120 tonnes per hour mineral water treatment system for a Dabie Mountain spring source, supporting a plant th...