

In today’s industrial and commercial sectors, water quality and filtration are critical to ensure the safety, consistency, and efficiency of production processes. From beverage manufacturing to high-precision industrial applications, the demand for advanced filtration solutions has never been higher. Membrane treatment systems have emerged as a versatile, efficient, and reliable solution for these needs, providing unparalleled precision in water and liquid purification.
Understanding Membrane Treatment Systems
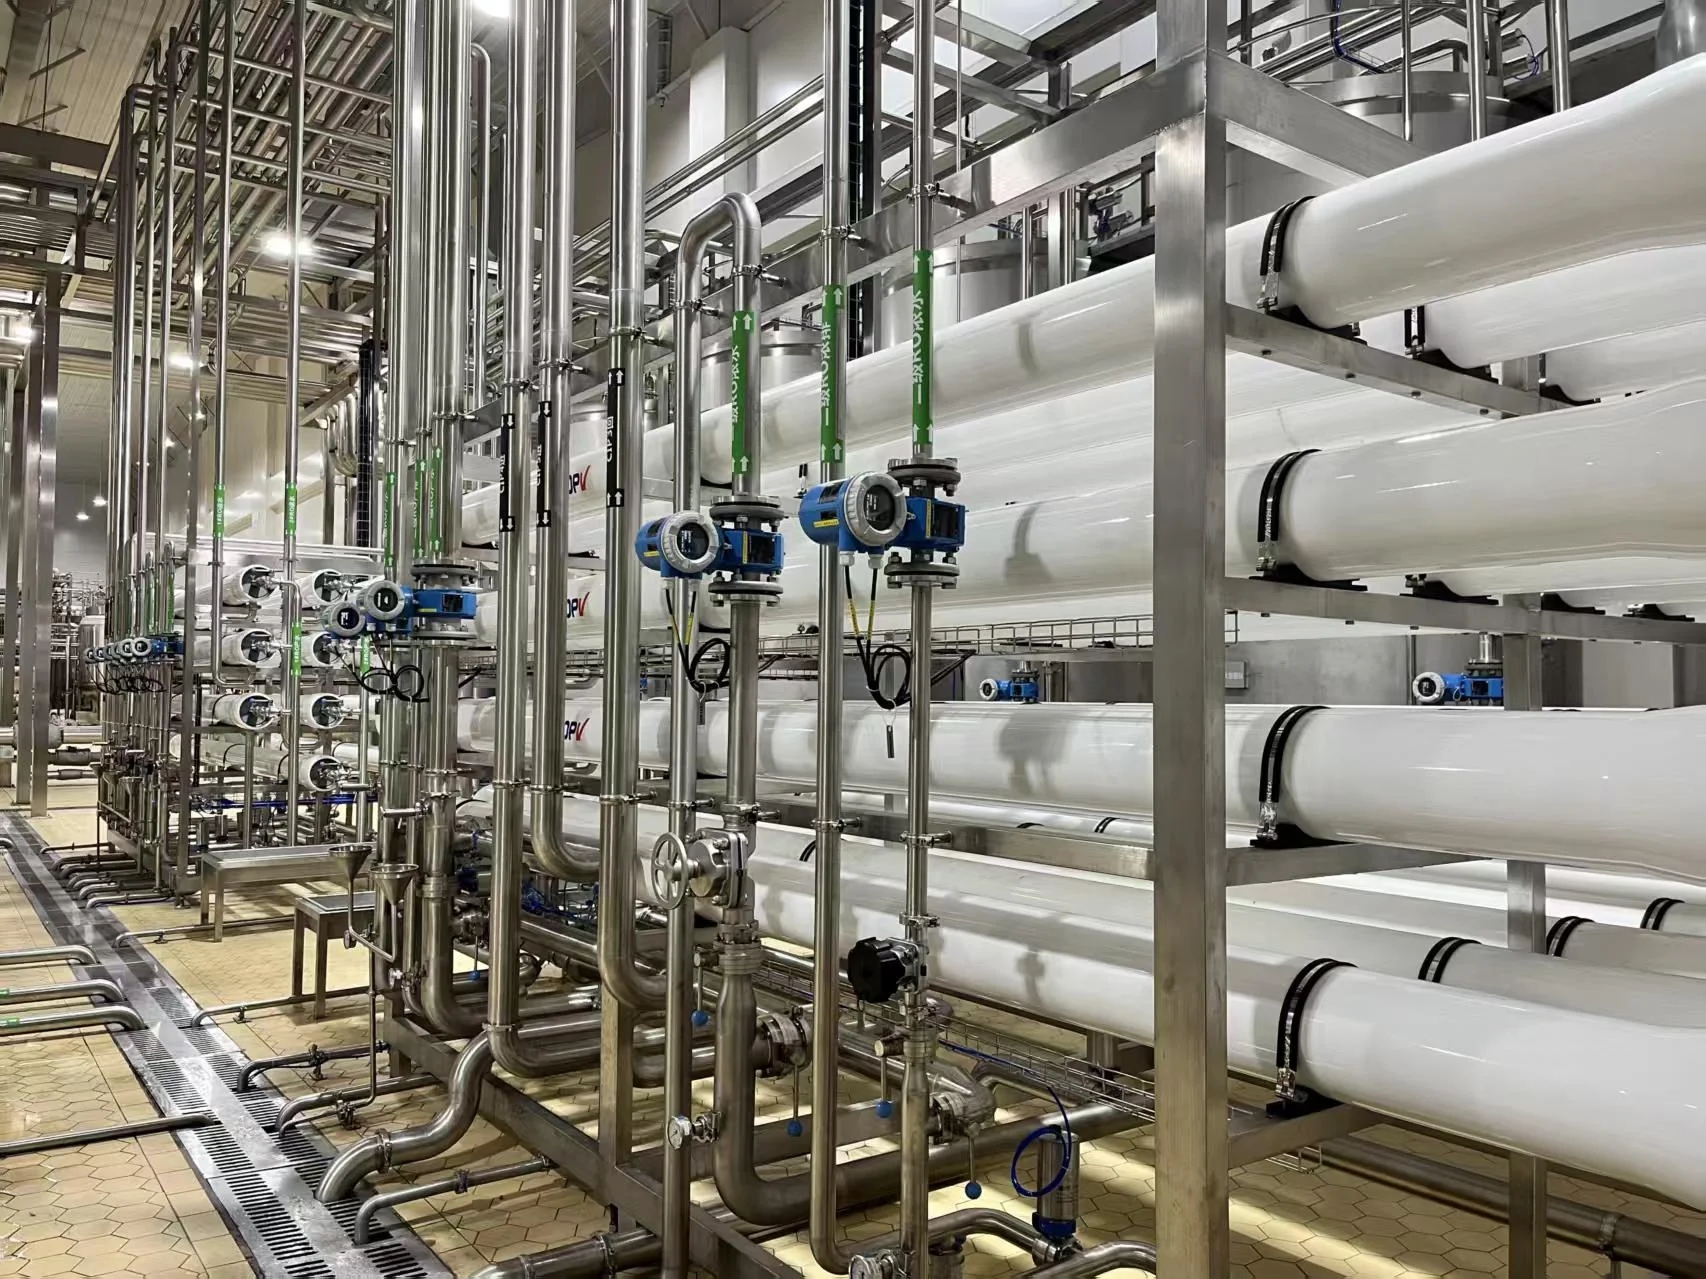
A membrane treatment system employs semi-permeable membranes to remove contaminants, particles, and microorganisms from liquids. Unlike traditional filtration methods, which rely on physical sieving or chemical treatment, membrane systems work at a molecular level, allowing only specific molecules—such as water—to pass through while retaining impurities.
There are various types of membrane filtration technologies, including microfiltration (MF), ultrafiltration (UF), nanofiltration (NF), and reverse osmosis (RO). Each has a specific application depending on the size of particles to be removed and the quality of water required.
-
Microfiltration (MF): Ideal for removing suspended solids and bacteria.
-
Ultrafiltration (UF): Removes viruses, macromolecules, and fine particles.
-
Nanofiltration (NF): Softens water and removes divalent and multivalent ions.
-
Reverse Osmosis (RO): Provides high-purity water by removing almost all dissolved salts and contaminants.
Advantages of Membrane Treatment Systems
-
High Efficiency and Reliability
Membrane systems consistently deliver high-quality water, ensuring that production processes are not compromised. By targeting contaminants at the molecular level, they minimize the risk of bacteria, pathogens, and scale formation, which are common challenges in beverage and industrial production. -
Environmental Sustainability
Membrane treatment significantly reduces the need for chemical treatment, lowering environmental impact and reducing chemical handling risks. Many modern systems are designed to conserve water and energy, aligning with global sustainability standards. -
Scalability and Flexibility
Whether a facility requires a small-scale filtration system or a large industrial setup, membrane systems can be scaled accordingly. Modular designs allow for easy expansion or integration with existing equipment. -
Cost-Effectiveness in the Long Run
Though the initial investment in membrane systems can be higher than conventional methods, the reduction in chemical usage, maintenance costs, and energy consumption makes them economically viable over time.
Application in Beverage Production
For beverage manufacturers, consistent water quality is essential. Impurities not only affect taste and shelf life but can also impact safety compliance. This is where companies like Pengxiang Huixing excel. Based in Shenzhen, China, Pengxiang Huixing offers comprehensive solutions spanning water treatment, beverage pre-treatment systems, PET blow-molding machines, filling and capping lines, labeling systems, conveying systems, and secondary packaging equipment.
By integrating advanced membrane treatment systems into beverage production lines, manufacturers can ensure:
-
Consistent Taste and Quality: Removal of chlorine, sediments, and organic compounds enhances the final beverage’s flavor and stability.
-
Operational Efficiency: Membrane systems minimize downtime caused by scale buildup or microbial contamination in production lines.
-
Regulatory Compliance: High-purity water ensures products meet international safety standards for bottled water, juices, carbonated drinks, and other beverages.
For more information about the solutions offered by Pengxiang Huixing, you can explore their membrane treatment system in detail.
Integration with Smart Factories
One of the defining trends in modern production is the move toward intelligent manufacturing. Pengxiang Huixing’s focus on smart workshop and smart factory planning ensures that their membrane treatment systems can seamlessly integrate into automated production environments.
This integration brings several advantages:
-
Remote Monitoring and Control: Sensors and IoT-enabled devices allow real-time monitoring of water quality, system performance, and maintenance needs.
-
Predictive Maintenance: AI-driven analytics can predict when membranes need cleaning or replacement, preventing unexpected downtime.
-
Enhanced Production Coordination: Water treatment processes can be synchronized with filling, packaging, and labeling operations, maximizing efficiency.
Industrial Cleaning and Safety Considerations
Maintaining membrane systems is critical to ensure long-term performance. Pengxiang Huixing provides on-site automated cleaning systems and industrial cleaning solutions that reduce manual intervention and enhance safety. Key maintenance practices include:
-
Regular Backwashing: To remove accumulated sediments and extend membrane life.
-
Chemical Cleaning: When fouling or scaling occurs, professional-grade cleaning agents ensure the membranes’ integrity is maintained.
-
Routine Inspections: Monitoring system pressure, flow rates, and water quality ensures optimal operation.
Through these measures, manufacturers can achieve a high level of hygiene, compliance, and operational efficiency.
Global Reach and Proven Expertise
With over 20 years in the beverage packaging and water treatment industry, Pengxiang Huixing has built a reputation for delivering high-performance equipment and end-to-end solutions. Their products have been exported to over a dozen countries including the UAE, Oman, Vietnam, the Philippines, and Malaysia. Domestically, their systems serve more than 20 provinces, demonstrating robust market trust.
Why Choose Membrane Systems with Pengxiang Huixing?
The combination of advanced membrane filtration technology and comprehensive industrial solutions makes Pengxiang Huixing a reliable partner for businesses aiming to improve water quality, production efficiency, and product consistency. Their approach emphasizes:
-
Innovation: Continuously introducing technologies from around the world and improving them for local conditions.
-
Integration: Offering complete solutions from water treatment to packaging, labeling, and logistics.
-
Certification and Quality: ISO9000 certified systems and recognition as a China High-Tech Enterprise.
This holistic approach ensures that clients not only meet production targets but also maintain high standards of quality and safety throughout their operations.
Conclusion
Membrane treatment systems represent a forward-looking, efficient, and environmentally responsible approach to water filtration. For industries where liquid quality is critical—especially beverage production—integrating these systems is no longer optional but a strategic necessity. Companies like Pengxiang Huixing provide not just equipment, but comprehensive solutions, ensuring that every step from water treatment to bottling and packaging operates at peak performance.
By leveraging smart, integrated, and sustainable technologies, businesses can achieve operational excellence, regulatory compliance, and consumer satisfaction. Investing in membrane treatment systems today means ensuring a safer, more efficient, and future-ready production process tomorrow.
Explore more about the solutions at Pengxiang Huixing’s membrane treatment system page to learn how advanced filtration can enhance your operations.