

As industries worldwide face increasing pressure to improve efficiency, reduce environmental impact, and ensure consistent product quality, membrane treatment systems have become a core technology across many sectors. From water purification to beverage processing and industrial cleaning, membrane-based solutions offer precision, reliability, and scalability that traditional methods often cannot match. In modern industrial environments—especially those pursuing intelligent manufacturing—membrane treatment systems are no longer optional components but strategic infrastructure.
This article explores the key applications of membrane treatment systems in modern industry and explains why they play such a vital role in integrated production and packaging solutions.
Understanding Membrane Treatment Systems
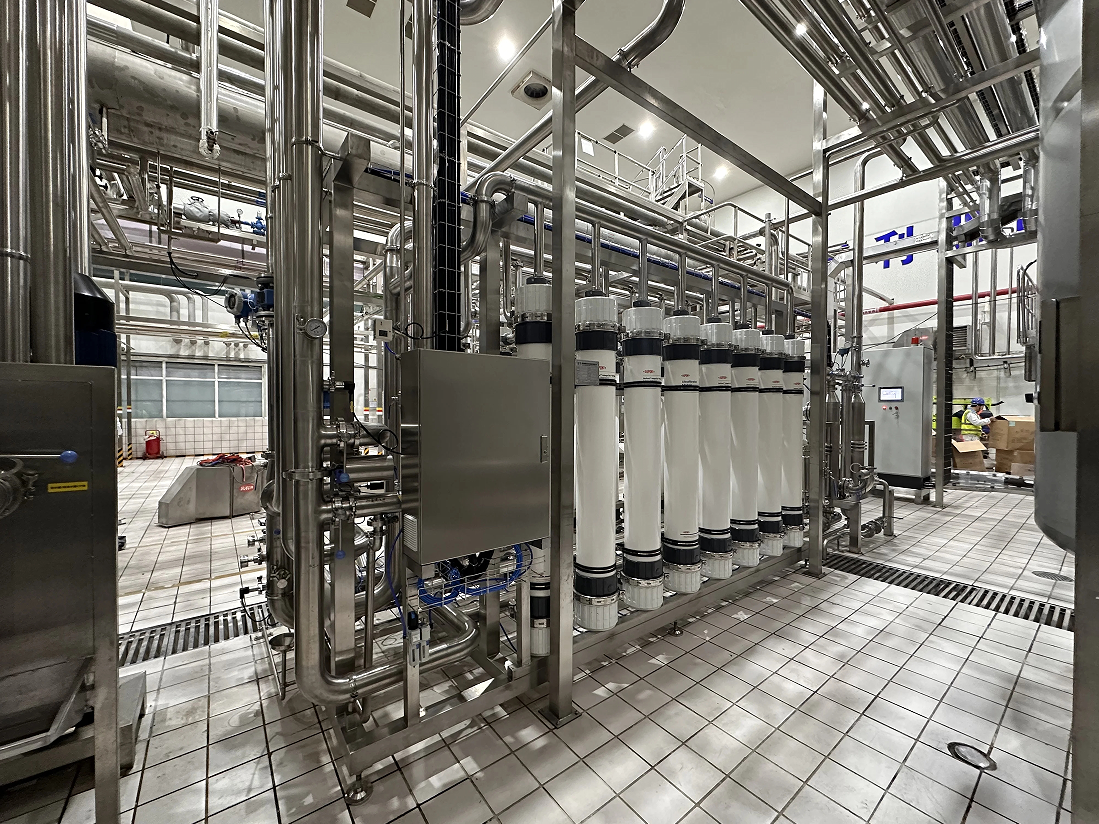
Membrane treatment systems use semi-permeable membranes to separate substances at the molecular or ionic level. Depending on pore size and operating pressure, common membrane technologies include microfiltration (MF), ultrafiltration (UF), nanofiltration (NF), and reverse osmosis (RO). Each type is designed for specific separation tasks, such as removing suspended solids, bacteria, organic compounds, or dissolved salts.
Compared with conventional filtration or chemical treatment, membrane systems offer higher accuracy, stable performance, lower chemical consumption, and easier automation—making them ideal for modern industrial processes.
Water Treatment and Purification
Industrial Process Water
Water is the backbone of most industrial operations, especially in food, beverage, and packaging manufacturing. Membrane treatment systems are widely used to purify raw water sources such as municipal water, surface water, or groundwater. Reverse osmosis and ultrafiltration systems remove impurities that could affect equipment performance or final product quality.
In beverage production lines, high-quality process water ensures stable taste, appearance, and safety. Membrane systems help manufacturers meet strict hygiene standards while maintaining consistent output.
Wastewater Recycling and Reuse
With rising water costs and stricter environmental regulations, many factories are adopting membrane systems for wastewater treatment and reuse. Membrane bioreactors (MBR) and advanced RO systems allow industrial wastewater to be treated and reused for cleaning, cooling, or auxiliary processes. This reduces overall water consumption and supports sustainable manufacturing goals.
Beverage and Food Processing Applications
Beverage Pretreatment Systems
In beverage production, water pretreatment is a critical step before mixing, carbonation, or filling. Membrane treatment systems remove microorganisms, colloids, and organic matter that can interfere with downstream processes. Compared with sand filters or carbon filters alone, membrane-based pretreatment delivers more consistent results and reduces the risk of contamination.
Integrated beverage pretreatment systems often combine membrane filtration with sterilization and automatic cleaning, ensuring stable production even at high capacities.
Ingredient Concentration and Clarification
Membrane technologies are also used to concentrate fruit juices, dairy ingredients, and flavor components without excessive heat. This helps preserve nutrients, color, and aroma. Ultrafiltration and nanofiltration systems are commonly applied for clarification and protein separation in juice and dairy processing.
Integration with Intelligent Manufacturing Lines
Modern factories are moving toward intelligent workshops and smart factories, where equipment, data, and workflows are highly integrated. Membrane treatment systems are increasingly designed to work seamlessly with automated production lines.
Pengxiang Huixing, based in Shenzhen, China, is a comprehensive beverage packaging machinery manufacturer that integrates membrane treatment systems into complete production solutions. From water treatment and beverage pretreatment systems to PET blow molding equipment, blow-fill-cap and blow-label-fill-cap production lines, labeling systems, conveying systems, and secondary packaging equipment, the company provides end-to-end solutions covering procurement, production, packaging, warehousing, logistics, distribution, and final consumption.
By embedding membrane treatment systems into intelligent production lines, manufacturers can achieve centralized monitoring, automated control, and predictive maintenance—key elements of smart factory design.
Cleaning and Sterilization Systems
Clean-in-Place (CIP) Systems
Membrane treatment systems play a vital role in CIP and on-site automatic cleaning systems. High-purity water produced by RO or UF systems ensures effective cleaning without leaving residues that could affect product safety. In beverage and food factories, reliable CIP performance directly impacts hygiene compliance and production continuity.
Industrial Cleaning Solutions
In industrial cleaning applications, membrane systems help recover and reuse cleaning water, reduce chemical usage, and lower wastewater discharge. This not only cuts operating costs but also supports environmental responsibility.
Packaging and Filling Line Support
Membrane treatment systems indirectly support packaging and filling operations by ensuring consistent water quality for rinsing bottles, cooling equipment, and operating auxiliary systems. For high-speed bottling lines—such as bottled water production lines, juice and carbonated beverage lines, and gallon bottle production lines—stable water quality is essential for avoiding downtime and product defects.
Pengxiang Huixing’s core products include fully automatic bottle blowing, filling, and capping three-in-one machines, bottled filling and sealing production lines, and complete beverage production lines. When combined with reliable membrane treatment systems, these solutions help manufacturers maintain efficiency, hygiene, and product consistency at scale.
Industrial and Municipal Infrastructure Projects
Beyond food and beverage, membrane treatment systems are widely used in industrial parks, pharmaceutical manufacturing, electronics, and municipal infrastructure projects. High-purity water is required for cleaning, cooling, and process control in many advanced industries.
Membrane systems are particularly suitable for modular design, allowing capacity expansion as demand grows. This flexibility makes them ideal for long-term industrial planning and high-end factory design.
Advantages in Global Markets
As companies expand into international markets, compliance with global standards becomes essential. Membrane treatment systems help manufacturers meet diverse regulatory requirements related to water quality, hygiene, and environmental protection.
Pengxiang Huixing’s products have passed ISO9000 quality management system certification and the company has been recognized as a Chinese high-tech enterprise. With over 20 years of experience in beverage packaging machinery technology, its solutions are exported to regions including the UAE, Oman, Vietnam, the Philippines, and Malaysia. Reliable membrane treatment systems are a key part of this global success, supporting consistent performance across different water sources and operating conditions.
Accessing Advanced Membrane Solutions
For manufacturers seeking proven membrane treatment solutions integrated with modern production and packaging systems, more information can be found at:Membrane treatment system.
This resource provides insights into membrane treatment system configurations designed for beverage, industrial, and intelligent factory applications.
Conclusion
Membrane treatment systems have become indispensable across modern industries. From water purification and beverage pretreatment to cleaning systems and intelligent manufacturing integration, they deliver measurable benefits in quality, efficiency, and sustainability. As industrial operations become more automated and environmentally conscious, membrane technologies will continue to play a central role.
Companies that combine membrane treatment systems with comprehensive production and packaging solutions—supported by strong R&D, global experience, and intelligent factory planning—are well positioned to meet the evolving demands of modern industry.